
Sizing an industrial double spiral cooker for peak production
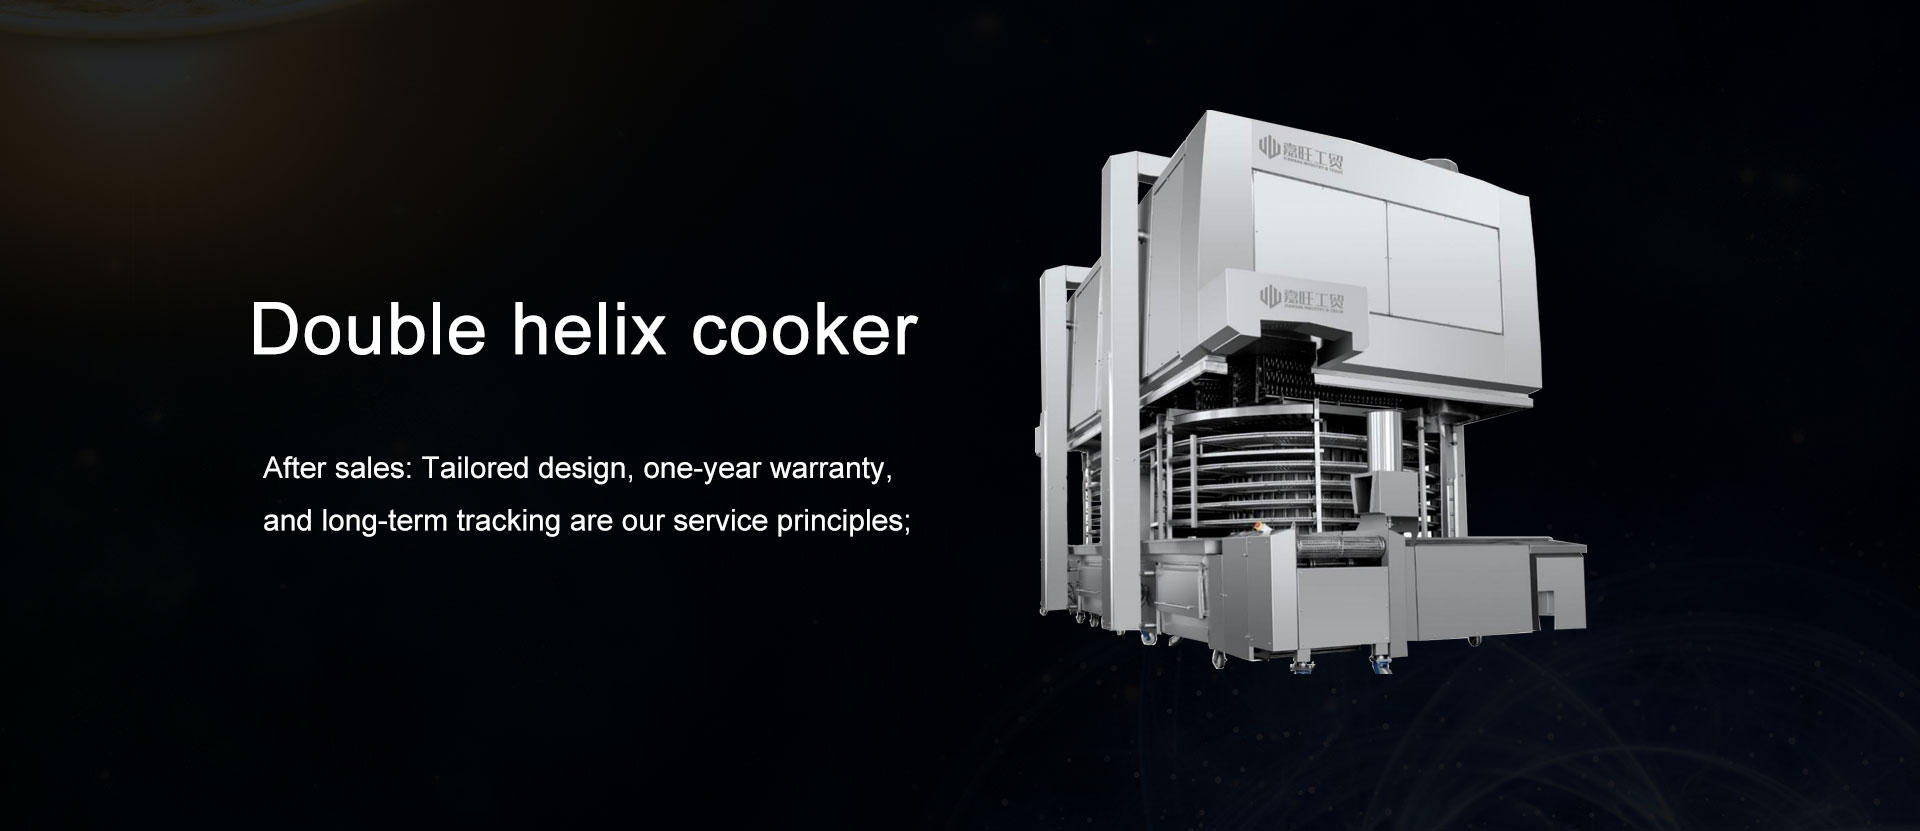
Size an industrial double spiral cooker around the product that places the greatest demand on belt space and cooking time at peak output. A quoted throughput is useful only when its assumptions match your product dimensions, loading pattern, inlet temperature, and required cooking endpoint. The selected machine must provide enough usable belt area, adequate heat delivery, and stable operation when the rest of the line is running at its busiest.
Start by separating three questions: how much product must pass through the cooker, how long it must remain inside, and whether the available utilities can support that load. A machine can satisfy the first two on paper and still miss production targets if steam pressure falls or products arrive unevenly.
Define peak demand as a production condition
Daily tonnage alone is a poor sizing input. Establish the required output during the actual production window, excluding planned cleaning, changeovers, and startup. Then distinguish the sustained rate from short bursts caused by upstream equipment. A cooker sized for average demand may struggle when preparation equipment releases product in concentrated batches.
Keep the mass basis consistent. If the target is packaged cooked weight, convert it to the corresponding cooker inlet rate using the expected process yield. Moisture loss or gain changes the relationship between inlet kilograms and saleable output. Comparing a supplier’s inlet capacity with your finished-product target can produce a misleading result.
Build a sizing sheet for the products expected to run during peak periods. Include:
- Required inlet throughput and duration of the peak run.
- Piece weight, dimensions, thickness variation, and permitted spacing.
- Lowest expected inlet temperature and required cooking endpoint.
- Validated residence time under the proposed cooking conditions.
- Loading restrictions, such as single-layer placement or separation between pieces.
The heaviest product is not automatically the limiting one. A lightweight, broad product may consume more belt area per kilogram, while a thicker product may need a longer residence time. Evaluate these cases separately rather than combining them into one average specification.
Connect belt loading, residence time, and throughput
The basic sizing relationship is straightforward: throughput equals the usable loaded belt area passing through the cooker per hour, multiplied by the product mass carried per unit area. Increasing belt speed raises potential throughput, but it also shortens cooking time.
For a continuous conveyor, the following relationships provide a useful first check:
Residence time = effective cooking belt length ÷ belt speed
Inlet throughput = usable belt width × belt speed × allowable loading density
Use consistent units. If length and width are in metres, belt speed is in metres per minute, and loading density is in kilograms per square metre, multiply the throughput result by 60 to obtain kilograms per hour.
Combining these relationships shows why a longer required cook time increases the necessary belt area at a fixed throughput. However, allowable loading density must come from a workable product arrangement. It cannot simply be increased until the calculation fits a smaller machine.
For individual pieces, derive loading from the number of lanes across the belt, the spacing along each lane, and piece weight. Include clearance at the belt edges and any spacing needed to prevent sticking, deformation, or restricted heat exposure. Nominal belt width can overstate capacity when the product does not fit neatly into the available lanes.
Use the belt length that contributes to the required cooking exposure. Transfers and sections outside the controlled cooking environment should not automatically count toward residence time. Likewise, a double spiral arrangement does not inherently double throughput: two spirals connected in series extend the product path, whereas independent paths require a different capacity calculation. Ask for a conveyor layout showing the actual route.
Check whether the cooker can heat the full load
Belt capacity establishes whether the product fits. Thermal capacity establishes whether it cooks correctly at that loading. The heat requirement depends on inlet mass flow, product temperature rise, moisture behavior, and losses through the enclosure, openings, and exhaust.
For a steam-based system, available steam pressure and flow at the machine matter more than the boiler’s nameplate rating. Other users may draw steam during the same production period. Distribution losses, control valves, and condensate removal also affect the conditions reaching the cooker.
A useful quotation should identify steam requirements at the specified product load and the required conditions at the connection point. Separate normal running demand from startup demand so the utility system can be assessed for both. Include electricity, water, drainage, and ventilation requirements in the same review.
Cooking uniformity needs its own check. Chamber temperature does not establish that every product has reached its required internal condition. Product thickness, inlet temperature, loading pattern, and heat distribution can all affect the slowest-heating pieces. For food safety applications, establish the required process with the responsible food safety team and validate it using representative product measurements.
Increasing belt loading can change exposure and airflow or steam circulation. Trials conducted with a lightly loaded belt therefore provide limited evidence for peak capacity. The intended maximum loading pattern must be part of the performance assessment.
Find the limits elsewhere in the line
The cooker’s rated output has little value if feeding equipment cannot maintain the planned spacing. Uneven deposits, overlapping pieces, or gaps between batches change both usable capacity and thermal load. Review the transfer arrangement, product orientation, and feed control before committing to belt width.
On a line that includes a coater for flat food, define where coating occurs and how that stage affects product dimensions, spacing, and transfer requirements. Compatibility depends on the actual process sequence and product condition; the equipment name alone does not establish a suitable combination.
Downstream capacity deserves equal attention. Cooling, freezing, or packaging must accept the cooker’s sustained discharge rate. If a packaging stoppage forces the cooking conveyor to stop, product may remain exposed beyond its intended residence time. Establish how the line handles interruptions, including controlled discharge, diversion, and product disposition where appropriate.
Space assessment should include access for cleaning, belt maintenance, utilities, and product transfers. A compact spiral footprint can still require substantial working clearance and installation height. Compare the complete installed layout rather than the enclosure dimensions alone.
Choose an operating margin with a clear purpose
Extra capacity is useful when it covers an identified condition: variation in product size, a defined future volume increase, or realistic fluctuations in feed rate. An arbitrary oversized machine can add capital cost, utility demand, and cleaning burden without improving usable production.
Check how the proposed cooker operates at both peak and routine demand. Lower throughput may require reduced loading, adjusted belt speed, or different cooking settings. Slowing the belt changes residence time, so it cannot be treated as a neutral adjustment. The supplier should explain the workable operating range for each important product.
If peak demand occurs only briefly, compare a larger unit with changes to production scheduling or parallel capacity. A double spiral cooker is most compelling when the process needs substantial continuous residence time within a constrained footprint. For short cooking cycles or frequent small batches, a steam tunnel or steam cabinet may warrant comparison, provided it can meet the product and handling requirements.
Make capacity acceptance measurable
Before comparing prices, give suppliers the same product data and request performance against the same conditions. Each proposal should state the loading pattern, inlet throughput, residence time, utility demand, and product endpoint behind its capacity claim.
Use a product trial to assess the limiting recipes at the intended loading. Record inlet temperature, belt speed, loading consistency, product temperatures, yield, and quality across relevant belt positions. Include an operating period long enough to observe stable conditions rather than relying only on the first acceptable samples.
Agree on acceptance criteria before ordering. These should cover sustained saleable output, cooking consistency, allowable product damage, utility consumption under defined conditions, and response to normal line interruptions. Select the machine that meets those conditions with a justified margin. The decisive figure is the output your complete line can maintain while producing acceptable product.
Online Consultation