
Electrical Fryer Factory Audit Checklist for Production Capacity and Quality Control
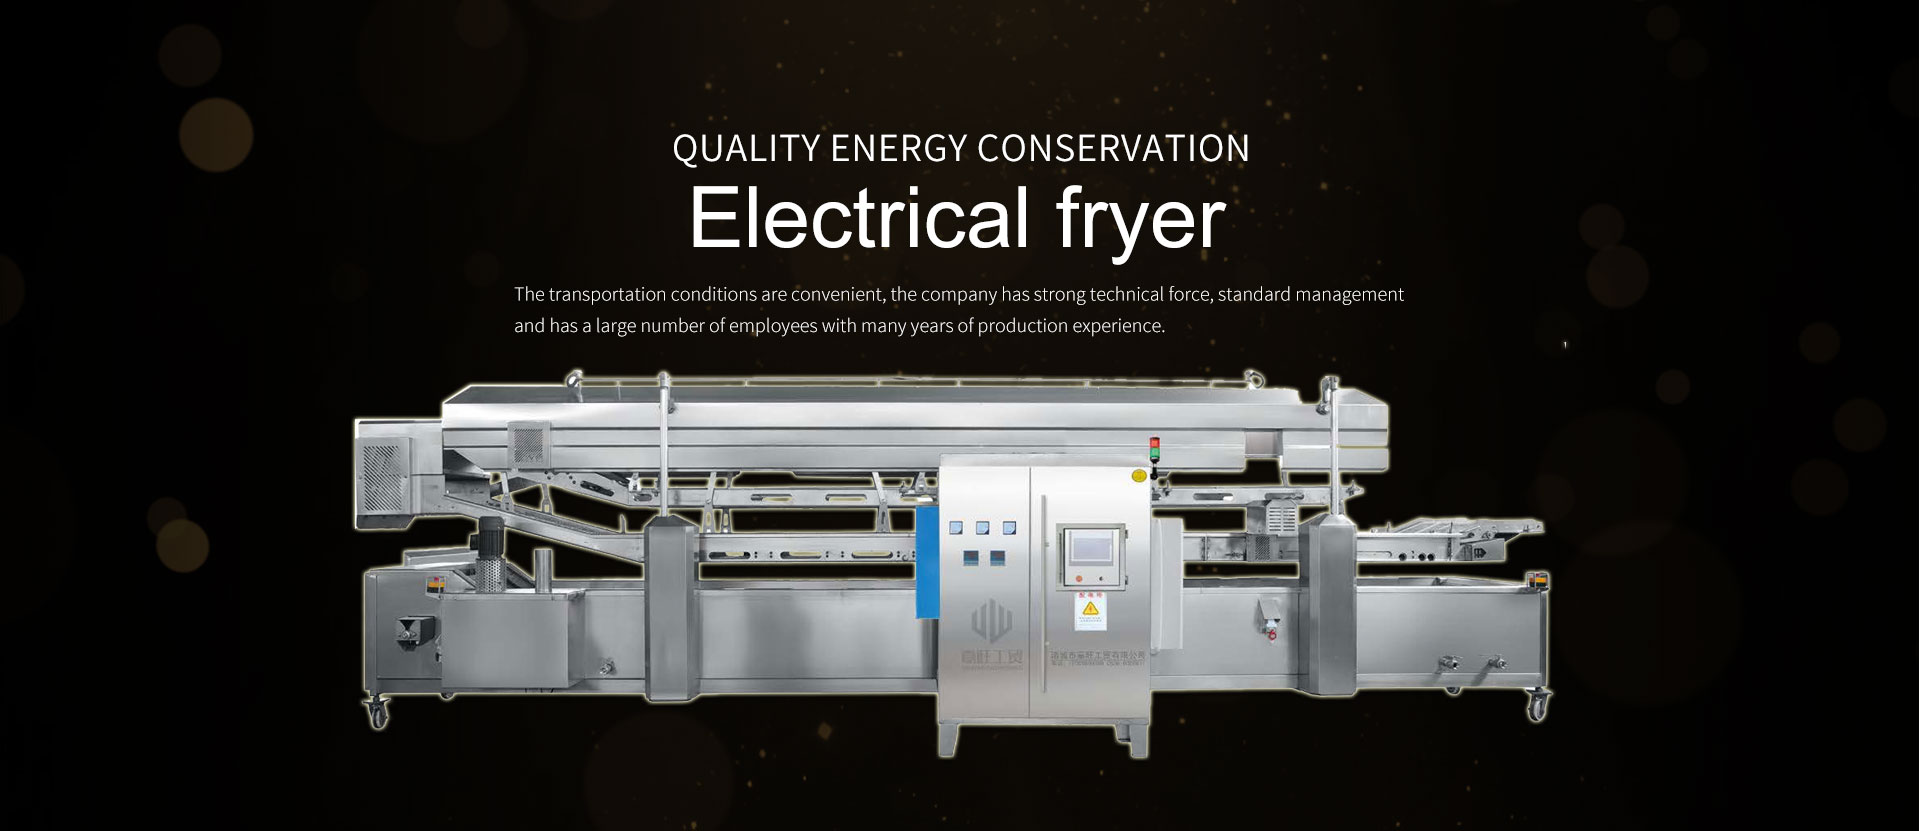
An electrical fryer factory audit should confirm whether the plant can repeat the same machine build under pressure, not simply whether it can assemble a sample unit that looks acceptable on the inspection day. In baking equipment projects, capacity claims often appear reasonable until the review reaches welding consistency, heating system sourcing, control cabinet assembly, and final test records. A useful audit starts on the shop floor, where material flow, component storage, and in-process identification reveal whether the factory works from a controlled routine or from temporary coordination.
Look at production capacity through bottlenecks
Nameplate output is less useful than actual bottleneck control. For an electrical fryer factory, the limiting stage may sit in sheet metal cutting, tank forming, immersion heater installation, electrical wiring, or leak and temperature testing. If stainless steel shells are stacked unfinished while only one technician handles wiring, stated monthly volume may depend on overtime rather than stable throughput. It also helps to see whether fryer bodies, oil contact parts, and insulated panels move in a clear sequence with work orders attached. When batches wait between fabrication and assembly for too long, distortion, part mix-up, and surface damage become more likely.
Pay attention to how the factory separates custom work from standard builds. A site producing mixed equipment, such as conveyors or a Steam tunnel machine, may have broad fabrication capability, but shared labor and tooling can create scheduling conflicts if the same team handles fryer tanks, steam housings, and electrical cabinets in parallel. This is not automatically a problem; it becomes one when planners cannot show a realistic production queue or when purchased parts arrive without allocation control.
Materials and thermal parts need direct verification
Electrical fryers depend heavily on oil-contact material quality and heating stability. During the audit, review the actual grades used for inner tank sections, covers, filter interfaces, and drain zones instead of relying on generic statements about stainless steel. Surface finish matters because rough weld areas and poor grinding make cleaning harder and can hold carbonized oil residue. Heater mounting points should be rigid, accessible for maintenance, and arranged so local overheating is less likely if oil circulation is uneven.
Temperature probes, contactors, solid-state switching parts, over-temperature protection, and cable routing deserve close attention. The issue is not whether these components exist, but whether they are installed with service access, labeling discipline, and heat separation from oil vapors. A crowded electrical box with inconsistent terminal marking usually signals weak assembly control. If the factory builds equipment for humid or hot production rooms, ask how they adapt sealing, ventilation, and cable protection to that environment.
Quality control should leave records, not explanations
A capable factory usually shows traceable inspection points across fabrication, assembly, and final testing. Weld inspection may be visual, but it should still follow a defined acceptance habit. Flatness of the tank top, alignment of lids, fit of baskets or conveying parts, insulation closure, and drain valve sealing all need verification before the machine reaches test power. Final testing should cover heating response, temperature control behavior, emergency stop function, abnormal alarm logic if fitted, and a hold period long enough to expose unstable wiring or sensor drift.
Ask to see how nonconforming parts are isolated. If rejected heaters, scratched panels, or faulty controllers remain mixed with released stock, the risk is practical and immediate. Rework control is equally important. A fryer repaired after leak test or electrical failure should be re-tested under the same release standard, not simply signed off after a quick adjustment.
Packaging, shipment, and installation readiness often expose hidden gaps
Large-volume orders fail in the last stage when a factory treats packing as an afterthought. Electrical fryer assemblies need protected probes, fixed movable parts, clear oil outlet protection, and moisture control for electrical sections if transit conditions are uncertain. Shipping marks should match machine identity records, especially when line projects contain multiple voltage options or left-right layout differences. Installation documents should reflect the real machine arrangement, utility connections, and maintenance clearances rather than a generic drawing set.
If the audit leaves one unresolved area, it is usually not appearance but control discipline. A clean workshop can still hide weak test routines, and a busy workshop can still produce stable equipment when routing, records, and release gates are well managed. The useful question is whether the factory can build the next ten electrical fryers with the same structure, wiring standard, and thermal performance as the unit shown during inspection.
Online Consultation